Direct OEM & distributor access to factory-traceable, high-bandwidth USB instrumentation, vector network analyzers, multi-slot modular mainframes, and calibrated RF verification units.
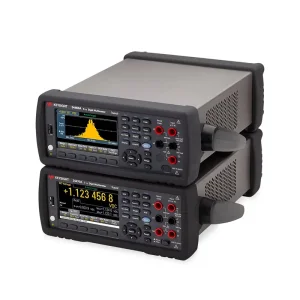
Modern engineering has shifted from proprietary benchtop racks to USB-driven modular architectures, blending portability with uncompromising measurement integrity.
Across semiconductor fabrication plants, aerospace ground testing, and consumer electronics manufacturing, the mandate for high throughput, physical space reduction, and cost efficiency has elevated USB instrumentation from supplementary convenience to core infrastructure. The modern USB test interface—spanning USBTMC (USB Test & Measurement Class), high-throughput USB 3.2 Gen 2x2, and USB4/Thunderbolt paradigms—delivers multi-gigabit throughput while operating as transparent endpoints within distributed Automated Test Equipment (ATE) environments.
As an international manufacturer, procurement aggregator, and authorized exporter, Machine-Win Technology Co., Ltd. bridge the gap between top-tier precision brands (including Keysight, Rohde & Schwarz, Tektronix, Keithley, and Druck) and worldwide testing facilities. We provide complete traceable procurement solutions that satisfy rigorous ISO/IEC 17025 metrology standards, guaranteeing low noise floors, documented signal integrity, and absolute factory authenticity across all exported instruments.
Analyzing the architectural shifts in physical layer protocols, high-speed power delivery, and edge instrumentation through 2030.
The universal adoption of Extended Power Range (EPR) up to 48V/5A demands specialized DC power analyzers and electronic loads capable of transient slew rate monitoring without introducing ground-loop distortion or thermal drift.
With bandwidth scaling to 80 Gbps and 120 Gbps asymmetric transmission, physical validation requires high-bandwidth real-time oscilloscopes, precision BERT fixtures, and vector network analyzers capable of resolving sub-picosecond skew and inter-symbol interference (ISI).
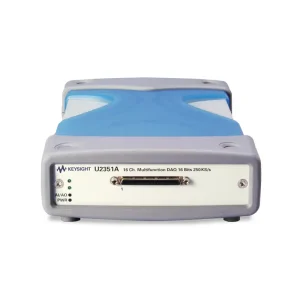
Decentralized data acquisition units, such as the Keysight U2300A Series, replace heavy chassis by digitizing analog sensors at the test point and transmitting packetized raw data directly over shielded USB bus structures.
Standardization of SCPI commands over high-speed USB hubs; full drop-in replacement for legacy GPIB/RS-232 rack instruments.
Inter-device clock distribution architectures that allow daisy-chained USB VNAs to synchronize within picosecond phase jitter limits.
Edge-embedded thermal and impedance auto-compensation algorithms running inside USB dongle analyzers to eliminate warm-up latency.
Total galvanic isolation between high-voltage automotive/grid equipment and host PCs using integrated fiber-optic USB active cabling.
Deploying robust, calibrated test equipment into mission-critical engineering pipelines around the globe.
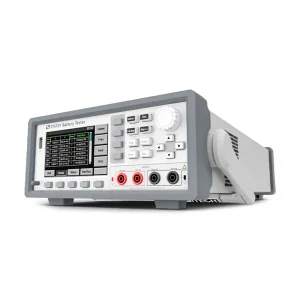
Utilizing high-precision Battery Testers (e.g., Itech IT5100 series) and multi-channel USB DAQs to analyze cell internal resistance, thermal runway indicators, and dynamic DC current waveforms during EV regenerative braking simulation.
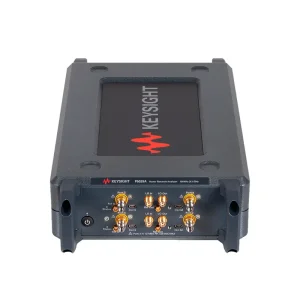
Streamline USB VNAs (such as Keysight P5004A) eliminate benchtop footprints in airport hangars, allowing field technicians to perform full 20 GHz 2-port S-parameter characterization of radar transmission lines and radomes directly on the tarmac.
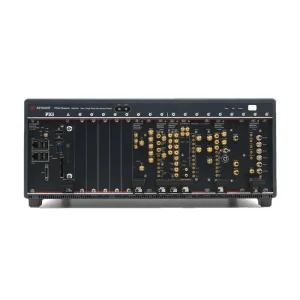
In cleanrooms, Keysight E5270B precision mainframes coupled with high-speed digital protocol exercisers trace micro-ampere leakage currents and validate advanced wafer-level device curves across wide temperature gradients.
Eliminating supply bottlenecks through strategic inventory consolidation, cross-brand compliance, and multi-hub logistics.
Procuring specialized test instrumentation presents high enterprise friction: lead times can extend past 40 weeks, configurations are prone to licensing mismatches, and multi-vendor import declarations introduce steep administrative overhead. Machine-Win Technology operates an engineered supply chain infrastructure headquartered in Hong Kong, with operational staging and technical test facilities across Shenzhen and Nanchang.
By leveraging an audited network of 2,000+ certified supply partners, we identify factory-original, serial-traceable stock for mission-critical instruments from Keysight Technologies, Rohde & Schwarz, Tektronix, Druck, Keithley, Fluke, ITECH, and Chroma. This enables project managers to consolidate their bills of materials (BOM)—ranging from high-end bit error ratio testers to basic USB sensor probes—into a unified commercial invoice with coordinated multi-unit transit.
Every piece of hardware dispatched through our export logistics pipeline undergoes rigorous pre-shipment quality verification (QA):
Factory-certified portable oscilloscopes, spectrum analyzers, compliant compliance testing suites, and battery cyclers ready for global dispatch.
Clear answers to procurement protocols, hardware validation, calibration compliance, and international logistics.